Sydney · 0402 531 010 Talk To Us
As a leading OEM/ODM manufacturer, our CE-certified machine trailers and expandable container modules are engineered for extreme structural reliability, high axial load capacities, and seamless international transport compliance. Explore our precision-manufactured product lineup designed for mobile living, heavy machine transport, site offices, and commercial deployment:
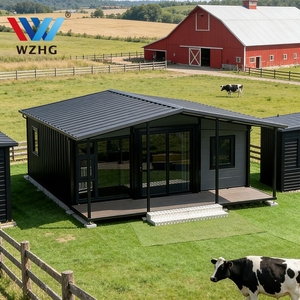
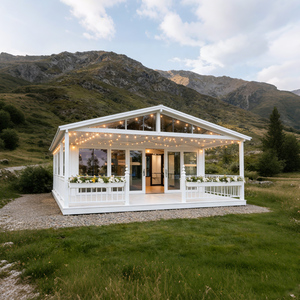
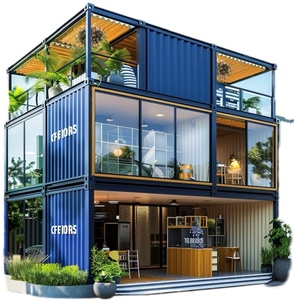
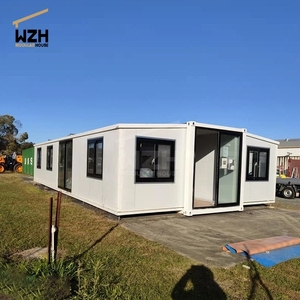
In modern industrial logistics and modular housing deployment, structural integrity is non-negotiable. As an established certified OEM/ODM manufacturer, our company engineers high-capacity machine trailers and expandable mobile structures adhering strictly to CE Certificate EN 1090-1:2009+A1:2011 (Execution of Steel Structures) and ISO 3834-2 welding quality management. Unlike basic regional suppliers, our mobile chassis integrated units are developed to withstand extreme dynamic loading during transit, as well as prolonged environmental stress on rugged Australian, Pacific, European, and North American job sites.
Every trailer frame and expandable container base leaves our production line with a heavy-duty, hot-dip galvanised structural steel chassis (Q235B / Q355B grade high-tensile steel). This process guarantees a minimum coating thickness of 85 µm, providing superior protection against atmospheric corrosion, salt spray, and moisture ingress. Whether utilized for heavy plant equipment transport, mobile generators, or supporting multi-room expandable luxury villas, our structural framework prevents sagging, torsional twisting, and floor deflection over decades of service life.
Robotic MIG welding ensures flawless joint penetration across primary load beams, preventing structural fatigue under heavy payload vibrations.
Braking systems, lights, safety couplings, and axle ratings engineered to meet rigorous EU Machinery Directives and Australian ADR standards.
Integrated dual-hydraulic or hand-winched accordion folding walls allow a 20ft or 40ft container platform to fully open in less than 2 hours.
To assist procurement directors, mining logistics managers, and commercial modular developers, the matrix below outlines core engineering tolerances, material specifications, and regulatory standards applied across our manufacturing facility:
| Specification Parameter | 20ft Standard Machine Platform | 20ft Premium Expandable Unit | 40ft Heavy Duty Expandable Villa |
|---|---|---|---|
| CE Structural Standard | EN 1090-2 Class EXC2 | EN 1090-2 Class EXC2 | EN 1090-2 Class EXC3 Heavy Industrial |
| Main Beam Material | Q355B Hot-Rolled Channel Steel | Q355B Heavy Steel Section | Reinforced I-Beam Structural Steel |
| Corrosion Protection | Hot-Dip Galvanized (85µm) | Hot-Dip Galvanized + Polyurethane Paint | Marine-Grade Epoxy Zinc + HDG |
| Axle & Suspension Option | Dual Axle Mechanical Leaf Spring | Torsion Axle or Custom Trailer Chassis | Tri-Axle Air Suspension / Flat-bed Mount |
| Thermal Insulation | 50mm EPS / PU Sandwich Panel | 75mm High-Density PU / Glasswool | 100mm Rockwool (Fire Rating Class A) |
| Expanded Floor Area | Approx. 14.4 m² (Single Volume) | Approx. 36.5 m² (Three-in-One) | Approx. 72.0 m² (Multi-Bedroom) |
| Deployment Method | Direct Crane / Hiab Drop | 2-Person Manual Winch / Mechanical Jack | Integrated Hydraulic Expansion System |
As global supply chains place an increasing premium on mobility, rapid assembly, and strict carbon footprint accounting, the market for machine trailers and expandable container homes is undergoing a fundamental transformation. B2B procurement decision-makers are shifting away from traditional permanent structures toward relocatable, high-asset-value mobile assets.
Fuel economy regulations and towing capacity limitations (such as 3.5-tonne and 4.5-tonne highway towing caps in Australia and Europe) are driving manufacturers toward ultra-high-strength steel alloys. By incorporating advanced thermo-mechanically rolled steel, modern machine trailer chassis achieve up to a 25% reduction in dead weight (tare mass) without sacrificing structural tensile strength. This payload optimization enables commercial buyers to transport larger equipment or thicker wall insulation on standard commercial driver licenses.
Next-generation machine trailers and expandable site camps are rapidly adopting IoT telemetry systems. Real-time sensors track load distribution, tire pressure, brake shoe wear, and chassis vibration during transit across unpaved mining or agricultural roads. Furthermore, electro-hydraulic automatic leveling systems allow expandable units to level themselves on uneven site topography within minutes at the push of a single button, drastically reducing site labor costs.
Environmental regulations across the EU, Australia, and North America are mandating lower operational carbon emissions for remote site accommodation. Future-ready expandable trailers are now manufactured with factory-integrated solar roof channels, micro-inverter wiring loops, and thermal-bridge-free sandwich panels. These technological additions allow mobile units to operate autonomously off-grid, dramatically cutting down reliance on diesel generators on remote job sites.
The technical evolution of machine trailers over the past decade has moved from simple flatbed haulage frames to highly engineered, multi-functional modular platforms. Early trailer designs suffered from seal degradation, hinge binding during expansion, and poor insulation at structural seam joints. Today, advanced mechanical design tools—including Finite Element Analysis (FEA) dynamic loading simulations—have revolutionized trailer engineering.
Continuous marine-grade EPDM rubber seals ensure zero water penetration or air leakage, even during driving rain and high winds up to 120 km/h.
Heavy-duty stainless steel piano hinges and custom drop-forged pivots undergo 10,000+ cycle stress tests to guarantee zero binding over the product lifespan.
Factory-installed conduit channels for electrical wiring, plumbing lines, and data cabling eliminate the need to cut into structural panels on site.
This focus on refined structural engineering guarantees that every unit—whether deployed as a mobile machinery workshop, a specialized horse float trailer, or a multi-bedroom luxury container villa—operates reliably in the field with minimal maintenance requirements.
Below are authoritative engineering and procurement answers addressing common queries from commercial buyers, fleet managers, and international distributors:
With dedicated sales engineering hubs in Sydney, Melbourne, and New Zealand, alongside our state-of-the-art automated manufacturing facility, we offer global partners unprecedented quality control, rapid delivery schedules, and direct factory pricing. Whether you require a fleet of heavy-duty machine trailers, specialized horse floats, or a bulk order of expandable container homes for land development, our engineering team is ready to support your technical drawings and volume specifications.
Speak directly with our technical engineering team regarding custom trailer configurations, CE compliance documentation, bulk wholesale pricing, or lead times.