Sydney · 0402 531 010 Talk To Us
Factory-direct precision engineered mobile offices, expandable container structures, and multi-storey commercial units built for rapid global deployment and demanding site conditions.
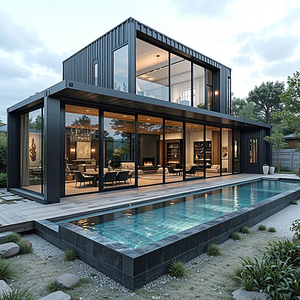
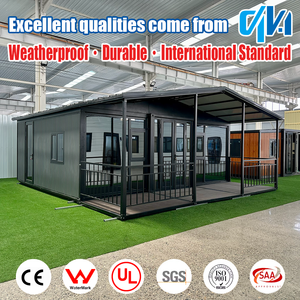
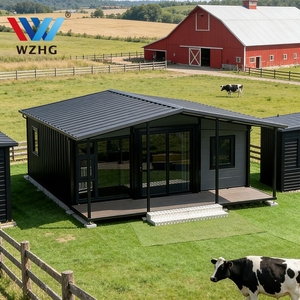
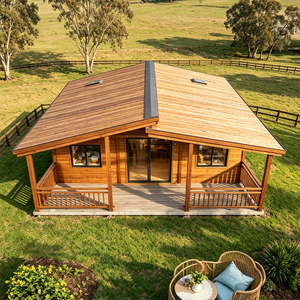
An authoritative technical analysis on structural compliance, offsite automation, and OEM customisation frameworks for commercial developers and remote site operators.
Our custom mobile offices leverage cold-formed Q355B high-tensile structural steel profiles. Chassis structures undergo continuous submerged arc welding and hot-dip galvanisation with a minimum zinc coating thickness of 275 g/m² (Z275). This ensures mechanical structural stability against flexural stress during frequent crane lifts and rough-terrain logistics transport.
Featuring high-density Polyurethane (PU) core or non-combustible Rockwool sandwich wall panels ranging from 75mm to 100mm, our buildings achieve thermal resistance values exceeding R-4.2 m²·K/W. Double-glazed argon-filled low-E glass aluminum window frames prevent thermal bridging, drastically reducing field HVAC energy consumption by up to 38% in extreme climates.
All Mechanical, Electrical, and Plumbing (MEP) systems are 100% prefabricated offsite within automated assembly jigs. Standardized conduit runs, pre-tested hydraulic distribution lines, and IP66-rated external utility hookup ports enable turn-key connection within hours of site positioning, eliminating specialized trade labor overhead on remote job sites.
“Transitioning from traditional field-built site offices to factory-controlled OEM mobile container systems reduces project execution timelines by 65% while establishing guaranteed compliance with strict international building codes (AS/NZS, IBC, and CE).”
| Structural Technical Parameter | Standard Commercial Mobile Office | Heavy-Duty Mining & Field Command Office |
|---|---|---|
| Primary Steel Sub-Structure | 2.5mm Cold-Rolled Galvanised Profile | 4.0mm Hot-Rolled Q355B Structural Channel |
| Floor Live Load Capacity | 2.5 kN/m² (Standard Office Load) | 4.5 kN/m² (Heavy Equipment & High Traffic) |
| Roof Snow / Load Rating | 1.5 kN/m² | 3.0 kN/m² Reinforced Deck Structure |
| Insulation Type & Thickness | 50mm EPS / Glasswool Panel | 75mm/100mm High-Density PIR or Rockwool |
| Fire Resistance Rating (FRR) | B1 Flame Retardant Class | Class A Non-Combustible (2-Hour Fire Rated) |
| Acoustic Isolation Index (Rw) | Rw = 32 dB (Noise Reduction) | Rw = 45 dB (High Acoustic Privacy) |
| Corrosion Protection Coating | Single-layer Polyurethane Spray (C2) | Epoxy Zinc-Rich Primer + Fluorocarbon Topcoat (C5-M) |
How global enterprise procurement managers, resource sector operators, and civil contractors are altering their capital deployment for relocatable asset infrastructure.
Modern B2B buyers are abandoning single-use, fixed temporary structures in favor of modular mobile offices that maintain high residual asset value. Multi-fold container offices allow corporate fleets to redeploy administrative assets across multiple project lifecycles spanning different geographical regions without structural degradation.
With strict Scope 1 and Scope 3 emissions reporting, industrialized offsite manufacturing reduces on-site construction waste by up to 90% and site traffic disruption by 70%. Enterprise buyers prioritize manufacturers utilizing recyclable steel, low-VOC interior coatings, and solar PV roof integration kits.
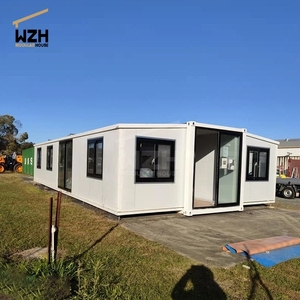
Containerized shipping economics drive design innovation. Advanced expandable container offices pack into standard ISO 20ft or 40ft High-Cube footprints. This allows up to 4 fully functional 34m² office units to be shipped in a single sea freight container, cutting international transport costs by 75% compared to rigid volumetric pods.
Factory-fitted smart infrastructure is now a standard OEM request. Mobile offices are outfitted with remote environmental sensors, automated occupancy HVAC controls, smart door access control, and pre-wired fiber optic backbones to ensure instant digital connectivity upon site drop.
Key technological breakthroughs changing how mobile offices are engineered, manufactured, and deployed.
Moving away from stark industrial site sheds, next-gen mobile offices incorporate warm wooden architectural veneers, indirect LED circadian lighting, and sound-absorbing acoustic ceiling baffles to boost field management productivity and wellbeing.
Integrated high-efficiency solar roof membranes, lithium battery storage banks, rainwater harvesting gutters, and self-contained greywater filtration systems allow deployment in remote exploratory regions without grid connections.
Patented hydraulic and mechanical winch systems allow a two-person installation crew to fully expand and structurally lock a 72m² mobile office facility in under 90 minutes without needing heavy crane hire.
Detailed technical answers addressing engineering customization, factory lead times, international transport logistics, and structural compliance certification.
Direct factory pricing, strict quality control, and comprehensive global logistics support for distributors, resource companies, and commercial builders.
By cutting out intermediate trading agents, enterprise procurement managers gain direct access to raw manufacturing cost structures, transparent material bills of quantity (BOQ), and volume tier pricing.
Every mobile office undergoes strict quality assurance before factory exit, including 24-hour high-pressure water spray testing for leak detection, structural deflection checks, and complete MEP circuit testing.
Our in-house architectural and structural engineering team provides 3D CAD modeling, BIM files, and photorealistic renderings during the pre-production phase to ensure exact design alignment.
Connect with our senior engineering and export sales specialists to receive custom structural layouts, technical spec sheets, and competitive volume price quotes for your project needs.